3D Printing Troubleshooting for Geometric Wall Art — Common Issues & Fixes
01 / GAPS IN THIN OR SINGLE-PERIMETER WALLS (CORAL SPONGE)
Solved in the updated Coral Sponge 3D models
All three Coral Sponge 3D models (Coral Sponge 01, 02 and 03 tileable) now have updated geometry. The walls are at least 1 mm thick everywhere, measured across the wall itself and not only in a horizontal cross-section. With a 0.4 mm nozzle and default slicer settings, at least two perimeters now fit in the wall, so the Coral Sponge now prints with default settings.

Why thin walls print with gaps
Some slicers struggle to generate continuous perimeters when a wall changes between:
- Thicker sections (2 or more perimeters)
- Thinner sections (1 perimeter, or close to the slicer’s minimum wall width)

Instead of creating one closed perimeter first and adding extra perimeters where there is space, these slicers generate two perimeters at once in thick areas and a separate single perimeter in thin areas. This leads to:
- Gaps in the wall
- Disconnected perimeters
- Weak or unstable 3D printed parts

Also, if a wall is thinner than the slicer’s minimum wall width, the slicer may skip the perimeter entirely.

The goal, in any slicer
✔ A continuous, closed perimeter
✔ At least one perimeter wherever the wall exists
✔ Smooth transitions between thin and thick wall sections

PrusaSlicer
PrusaSlicer generally produces the correct behaviour by default. It generates a fully closed perimeter first, adds extra perimeters only where the wall thickness allows, and handles thin-wall transitions more predictably.

Still seeing gaps in thin walls? Settings to check in Bambu Studio and Orca Slicer
If a similar issue appears on another 3D model with thin walls, these are the settings worth checking. They are suggestions, not guarantees. Every model and block is different, and you may need to adjust the values. To see them, enable Advanced or Expert mode.
- Wall generator: Arachne (varies the line width to fill thin and variable walls)
- Wall transitioning filter margin: 1000% (allows more aggressive smoothing between thick and thin walls)
- Wall transition length: 150% (extends the blending distance when the wall thickness changes)
- Minimum wall width: 150% (forces a perimeter even for very thin walls)
- Minimum feature size: 50% (stops small wall features from being discarded)
- Seam position: Random (avoids a visible seam line and reduces weak points)
Ensure vertical shell thickness: enabled

These settings work in combination. Changing only one may not be enough.
Reduce the outer wall line width. Under Quality → Line width → Outer wall, try for example 0.45 mm → 0.30 mm. In testing, I was able to print a single block with a hole just by reducing the line width, with all other settings at default (Wall generator: Classic).
02 / HOLES IN HOLLOW BLOCKS PRINTED WITH 1 PERIMETER (LED UPGRADE)
Hollow blocks printed with a single perimeter, for example for the LED upgrade, can come out with holes or gaps when the walls are too steep. A single perimeter has no second perimeter to support it. When the wall leans too far, the perimeter of one layer doesn’t overlap enough with the layer below to bond, and holes appear.

The fix: orientation and print strategy
Reorienting the blocks can significantly improve the print.
- Tilt the blocks and enable supports, so the problem wall prints at a slight angle. This increases the printable width of the wall and helps the slicer generate a continuous perimeter.
- Drag, drop and rotate the blocks in your slicer to find the best angle. This works for single blocks and grouped layouts, such as 4×4 arrays. Split the group after rotating if needed.
- Adjust the rotation to your printer’s cooling performance and print speed.
- Fine-tune the slicing with Detect Thin Walls, Shell Thickness and Extrusion Width.

When using supports
- Match the support overhang threshold angle to the tilt of the block.
- No infill is needed for these supports.
- Limit the support height with support enforcers, so supports only appear where they’re needed.
03 / PYRAMID APEX NOT SHARP
Pyramid-shaped blocks can be difficult to print with a sharp apex in the default upright position, and the tip can come out less sharp than the model.

The fix: print the pyramids on their side with Place on Face
Printing a pyramid on its side often improves the sharpness of the apex. In your slicer:
1) Drag & drop the individual blocks into your slicer (I’m using PrusaSlicer).
2) Use the Arrange function to distribute the blocks on the print plate.
3) Select one block, click the Place on Face tool and choose a side face of the pyramid. The block aligns automatically. Apply this to all the blocks.
04 / NUMBERED BLOCKS: UNREADABLE NUMBERS WHEN SCALED DOWN (ELEPHANT’S FOOT)
Numbered blocks have the block number built into the base. When you scale the model down, the numbers become small, and the first layer can be squashed so much (the “elephant’s foot” effect) that the number is hard to read.

Fix 1: Adjust Z live during the first layer and slow down
- Use your printer’s live Z adjustment (Z offset) while the first layer prints, so the first layer isn’t squashed too much. Raise the nozzle in small steps until the number is clearly visible.
- Slow down the first layer.

Fix 2: Print the first layer in a contrasting colour
The number is cut out of the block as a boolean difference. Add a colour change after the first layer(s), so the first layer and the following layers are different colours. The number then stands out more clearly.

Fix 3: Set the solid bottom pattern to Concentric
Change the solid bottom pattern (“Bottom surface pattern” in Bambu Studio and Orca Slicer, “Bottom fill pattern” in PrusaSlicer) to Concentric. It draws perimeters that follow the outline of the number, so the number is easier to see.
05 / LAYER STEPPING ON THE TOPS: PRINT BLOCKS UPSIDE DOWN FOR FLATTER TOPS
When printing blocks with inclined top surfaces, visible layer stepping can affect the finish. Printing the blocks upside down moves this stepping to the base, giving a smoother, flatter top surface.

Place on Face
Use the Place on Face function in your slicer to lay each block flat on its top surface. Simply rotating the block 180° is not enough.
To make the tops stand out, add a filament colour change in the first few layers. The Tips & Tricks page has the details.
06 / VISIBLE LAYER LINES: PRINT ORIENTATION FOR A SMOOTHER FINISH

For designs such as Whipping Cream and Floating Fumes, print the blocks vertically to get smoother layer stepping.
This matters most when you scale the model down. At the native size, layer stepping is less noticeable, but on a smaller print it becomes more visible, so vertical orientation is essential.
The template has since been refined. Block divisions now follow the curvature and are organised by colour. Vertical positioning is still the key to the best result.
-
3D Model
For 3D PrintingSTL • STEP • DWG
Twisted Box 01
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Random Pentagons (3x Colour Versions)
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG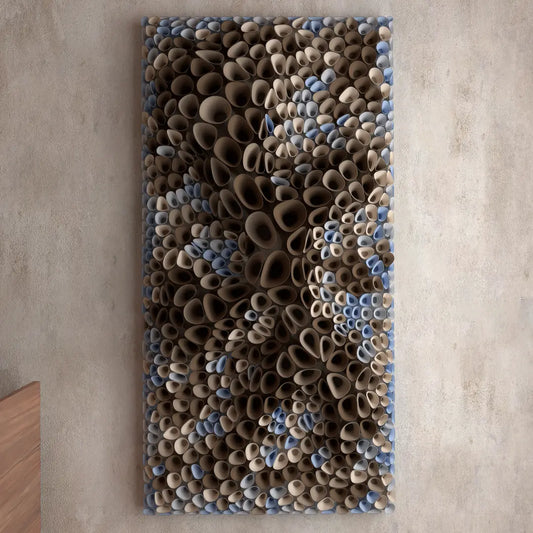
Coral Sponge 01
Regular price $18.54 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Triangle Wave
Regular price $16.69 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Floating Fumes
Regular price $13.91 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Whirl Peak
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Coral Sponge 03 (tileable)
Regular price $13.91 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Cracked Bulge
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Crater Ring
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG Sale
Spiral Ramp
Regular price $6.49 USDRegular priceUnit price per$9.26 USDSale price $6.49 USDSale -
3D Model
For 3D PrintingSTL • STEP • DWG Sale
Plunging Wave
Regular price $4.63 USDRegular priceUnit price per$9.26 USDSale price $4.63 USDSale -
3D Model
For 3D PrintingSTL • STEP • DWG Sold out
Mosaic (10 Blocks / 25 Layouts)
Regular price $20.39 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Twisted Box 03
Regular price $13.91 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Twisted Box 02
Regular price $11.59 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Whipping Cream
Regular price $13.91 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Tectonic Collision
Regular price $9.26 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Cornets de Fleur 02 (3× 22 blocks)
Regular price $11.13 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG Sale
Diagonal Wave
Regular price $11.13 USDRegular priceUnit price per$13.91 USDSale price $11.13 USDSale -
3D Model
For 3D PrintingSTL • STEP • DWG Sale
-
3D Model
For 3D PrintingSTL • STEP • DWG
Quarter Circle Waves
Regular price $13.91 USDRegular priceUnit price per -
3D Model
For 3D PrintingSTL • STEP • DWG
Paper Waves
Regular price $13.91 USDRegular priceUnit price per